SEARCH WHAT YOU WANT
Chemical Industry
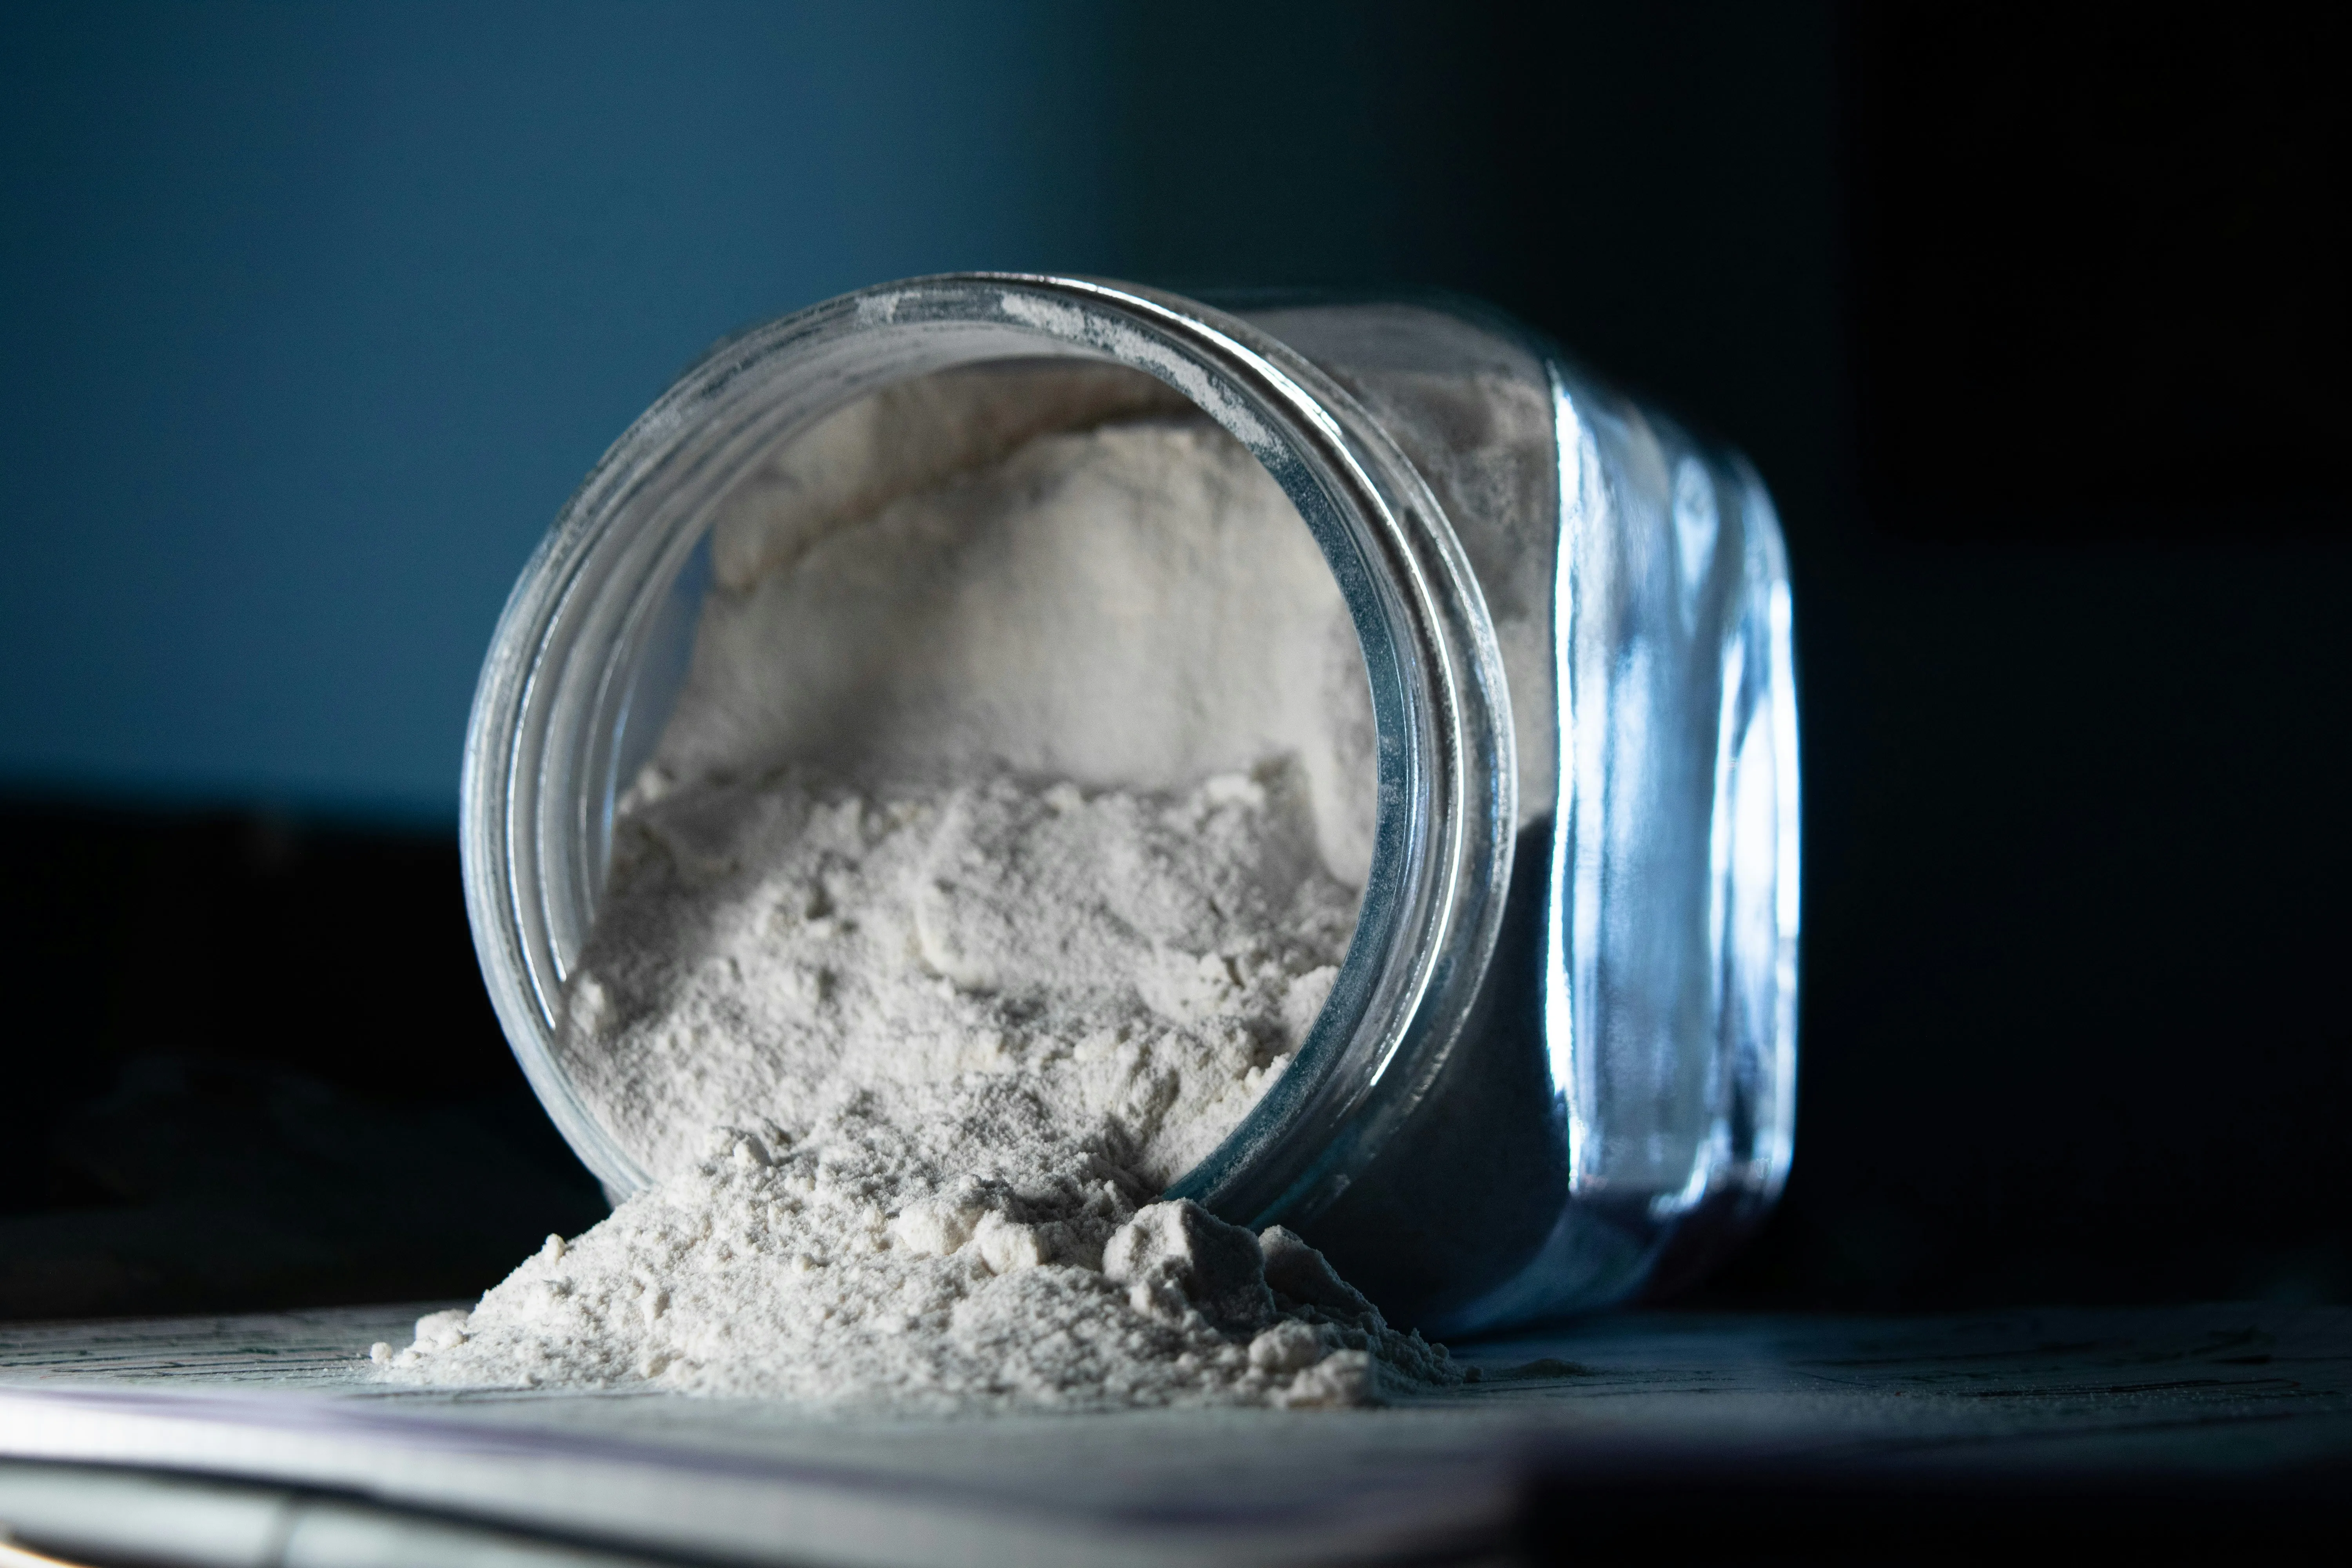
Engineered for durability and stability, our packaging machines handle various chemical products such as powders, granules, and liquids. With corrosion-resistant materials and reliable performance, they ensure safe, efficient, and consistent packaging in demanding environments.
Applicable Products:
Industrial powders, granules, liquids, detergents, chemical reagents.
Key Features:
● Corrosion-resistant materials suitable for harsh chemicals.
● Flexible packaging formats for different product types.
● Safety mechanisms to prevent leaks, contamination, and spills.
● High-speed multi-row and vertical packaging for large-scale production.
Benefits:
● Ensures safe, accurate, and consistent packaging.
● Reduces risk to operators and prevents product loss.
● Supports diverse chemical industries with customizable solutions.
Previous: Pharmaceutical Industry
Next: Daily Chemical Industry
Contact Us
Tel: +86 5911 8977
Phone: +86 187 2174 3221
Address: Building 20, No. 258 Yinlong Road, Jiading District, Shanghai, China.
Copyright © 2026 Shanghai Jieyu Intelligent Equipment Co., Ltd.